Key Takeaways
- A3 means higher flammability, not “mildly flammable”: ASHRAE 34 classifies R-290 (propane) and R-600A (isobutane) as Class A3: higher flammability with lower ignition energy and a wider flammable range than A2L refrigerants. They require different precautions from A2L refrigerants like R-454B, where ventilation is a recognized mitigation measure under the right conditions.
- Full nitrogen purge is mandatory before brazing: Flow-through nitrogen is not enough. Propane is heavier than air and pools in low spots inside the system. A complete evacuation and nitrogen fill eliminates the residual pockets that create flamethrower effects at leak points.
- Charge accuracy requires the pre-fill and re-zero technique: A3 systems carry critical charges, often under 150g. Pre-filling the charging hose with refrigerant, then re-zeroing the scale before opening to the system, eliminates the hose volume error that throws off small charges by several grams.
- Purpose-built hydrocarbon tools eliminate common failure points: Gas retention valves prevent refrigerant loss during gauge connection, 2mm small-diameter hoses minimize residual volume, and bottle-specific puncture valves handle the O-ring compatibility variations across R-290 cylinder brands.
A3 vs A2L: The Safety Gap Is Wider Than You Think
R-290, R-600A, and other hydrocarbon refrigerants carry ASHRAE 34 Class A3 classification.¹ That A3 designation means higher flammability: lower minimum ignition energy, a wider flammable range, and faster flame propagation than A2L refrigerants. R-290 behaves closer to the propane in your barbecue tank than to the R-454B in a residential heat pump.
The A2L safety framework most techs are learning right now does not transfer to A3 work. A2L refrigerants like R-454B have lower burning velocities and higher minimum ignition energies.¹ Under many field conditions, natural ventilation and airflow reduce A2L concentration below the lower flammability limit before ignition becomes likely. Understanding how refrigerant behaves in different states helps explain why A3 work requires different procedures.
Propane is heavier than air. It settles into low points: evaporator sections, compressor compartments, the bottom of a reach-in prep cooler. If the concentration falls within the flammable range (roughly 2.1% to 9.5% in air for propane), a pocket of R-290 in a low spot can ignite from a very small energy source, and the flame propagates rapidly through the gas stream.
European markets have run A3 systems for years, with systems growing larger and service ports becoming standard on bigger equipment.² In North America, A3 remains concentrated in small commercial refrigeration: prep tables, reach-in coolers, beverage units. Most of these systems ship with crimped-off connections and no service ports. But newer, larger equipment is arriving with standard service access, which means more field techs will be brazing, charging, and recovering A3 refrigerant. Techs building an A2L-ready toolbag need to understand that A2L-compliant tools do not automatically qualify for A3 work.
Not all A3 equipment is clearly labeled. Some units lack the red sleeve or flammable refrigerant sticker that has become standard. If a small, self-contained refrigeration unit has no nameplate identifying the refrigerant type, treat it as A3 until proven otherwise.
The Full Nitrogen Purge: Not a Flow-Through
Flowing nitrogen during brazing prevents oxidation inside the copper. On A3 systems, that flow-through alone is not enough.
Consider a prep table with an evaporator leak. The refrigerant has been vented (hydrocarbon refrigerants are exempt from EPA Section 608 venting prohibitions in approved SNAP end-use categories, including stand-alone commercial refrigeration equipment).³ Nitrogen flow is running through the system on the braze setting. The torch lights. And a two-inch flame shoots from the leak point.
That residual propane, pooled in a low section of the evaporator, hit the heat and ignited. The nitrogen was displacing gas as it flowed, but it had not purged the trapped pockets.
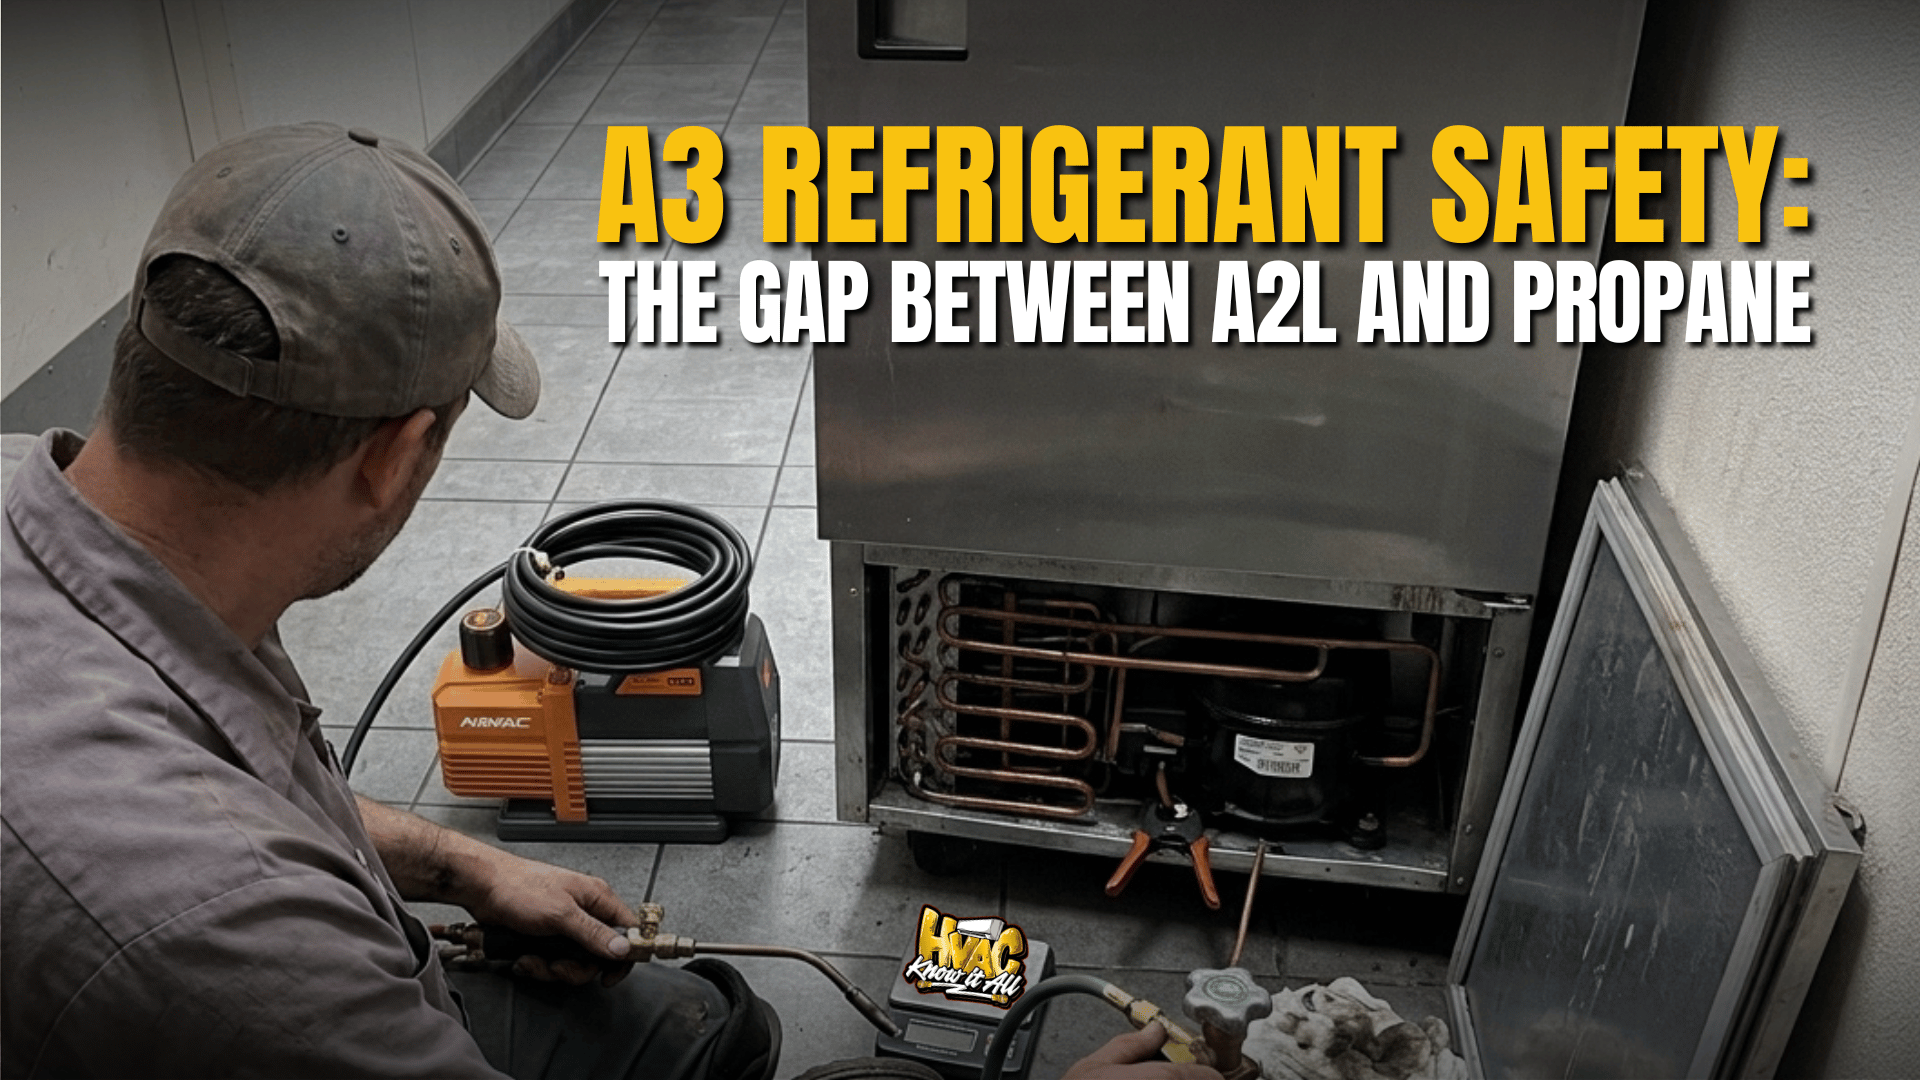
The fix is a full purge before brazing. Pressurize the system with nitrogen, vent it completely, and repeat. The goal is to evacuate every trace of hydrocarbon before a torch comes near the copper. Flow-through nitrogen for brazing protection starts after the purge is complete. This is a step beyond standard combustion safety analysis: it is hazardous gas management, not oxidation prevention.
Propane exhausting from the purge also settles. Vent it away from you, away from the torch, and away from the refrigerant cylinder. A concentration of vented propane near your torch tip or tank defeats the entire purpose of the purge.
Charging by the Gram: Pre-Fill, Re-Zero, Connect
A3 system charges are critical. A small prep table or reach-in cooler might hold 90 to 150 grams of R-290, though IEC 60335-2-89 permits charges up to roughly 500 grams for incorporated (self-contained) circuits.⁴ R-290 charging cylinders typically come in 10- to 14-ounce cans, and some small systems consume nearly an entire can. The margin for error is measured in single-digit grams.
The pre-fill and re-zero method eliminates the most common source of charging error on these small systems:
- Connect the charging hose to the system’s access point (either a brazed-in port or staple port) with the gas retention valve closed
- Open the cylinder valve to fill the hose with refrigerant
- Re-zero the scale after the hose is full
- Open the gas retention valve to begin charging the system
Without this step, the refrigerant that fills the empty hose registers on the scale as charge delivered to the system. On a 120-gram critical charge, a few grams of hose volume error is the difference between a properly charged unit and a callback.
The Yellow Jacket hydrocarbon kit uses 2mm small-diameter hoses specifically to minimize this residual volume problem. Larger quarter-inch hoses hold significantly more refrigerant between the cylinder and the system, amplifying the error if the pre-fill step is skipped. Even with small-diameter hoses, the pre-fill and re-zero technique remains essential for accurate system charging.
Purpose-Built Hydrocarbon Tools
The pinch-off tool is the most misunderstood component of A3 service work. On systems with crimped connections (still the majority in North America), the workflow is: charge the system, crimp the copper tubing flat with the pinch-off tool, leak check the crimp with liquid detector, and then braze the crimp closed.
The pinch-off tool must remain clamped during brazing. This is the step that catches techs. Copper relaxes when heated. A crimp that appears sealed will open slightly as the braze torch heats the surrounding copper, releasing propane directly into the flame. Keep the tool on, braze the joint closed, let it cool completely, then remove the clamp.
The gas retention valve (also called a Schrader core depression tool) serves double duty. On A3 work, it prevents charge loss during hose connection and disconnection. On any system, it eliminates the refrigerant spray that happens when connecting or removing hoses from a pressurized Schrader port. Back the stem out before disconnecting, and the Schrader core re-seats. The only refrigerant released is the small amount between the depressor and the core: a fraction of a gram rather than a blast of liquid or vapor.
Techs opening the kit for the first time also need to check O-ring compatibility with their R-290 cylinder brand. Approximately 60% of bottles on the market work with both O-rings installed in the puncture valve. The remaining 40% (including several common brands like EcoPure and National) require removing the top O-ring so the valve threads deeper onto the bottle. A second O-ring deeper inside the valve maintains the seal. A compatibility chart ships with the kit, and the removed O-ring goes back into the case for the next bottle that needs it.
The industry is moving toward larger A3 systems and standard service access. The transition from legacy refrigerants is not slowing down.⁵ Commercial refrigeration techs will encounter R-290 and R-600A more often. Working with these gases requires precautions for their higher flammability and explosion risk, beyond those used for mildly flammable A2L refrigerants. Have the tools ready and learn the techniques before your first A3 service call.
Additional Sources
- “Designation and Safety Classification of Refrigerants,” ASHRAE, Standard 34, 2024.
- “Refrigerating Systems and Heat Pumps: Safety and Environmental Requirements,” CEN, EN 378-1:2016+A1:2020.
- “Significant New Alternatives Policy (SNAP) Program: Substitutes in Refrigeration and Air Conditioning,” U.S. EPA, 2024.
- “Safety of Household and Similar Electrical Appliances: Particular Requirements for Commercial Refrigerating Appliances and Ice-Makers,” IEC, Standard 60335-2-89, Edition 3.0+COR3:2023.
- “Amendment to the Montreal Protocol on Substances that Deplete the Ozone Layer (Kigali Amendment),” UNEP, 2016.
Whether you require installation, repair, or maintenance, our technicians will assist you with top-quality service at any time of the day or night. Take comfort in knowing your indoor air quality is the best it can be with MOE heating & cooling services Ontario's solution for heating, air conditioning, and ventilation that’s cooler than the rest.
Contact us to schedule a visit. Our qualified team of technicians, are always ready to help you and guide you for heating and cooling issues. Weather you want to replace an old furnace or install a brand new air conditioner, we are here to help you. Our main office is at Kitchener but we can service most of Ontario's cities
Source link
